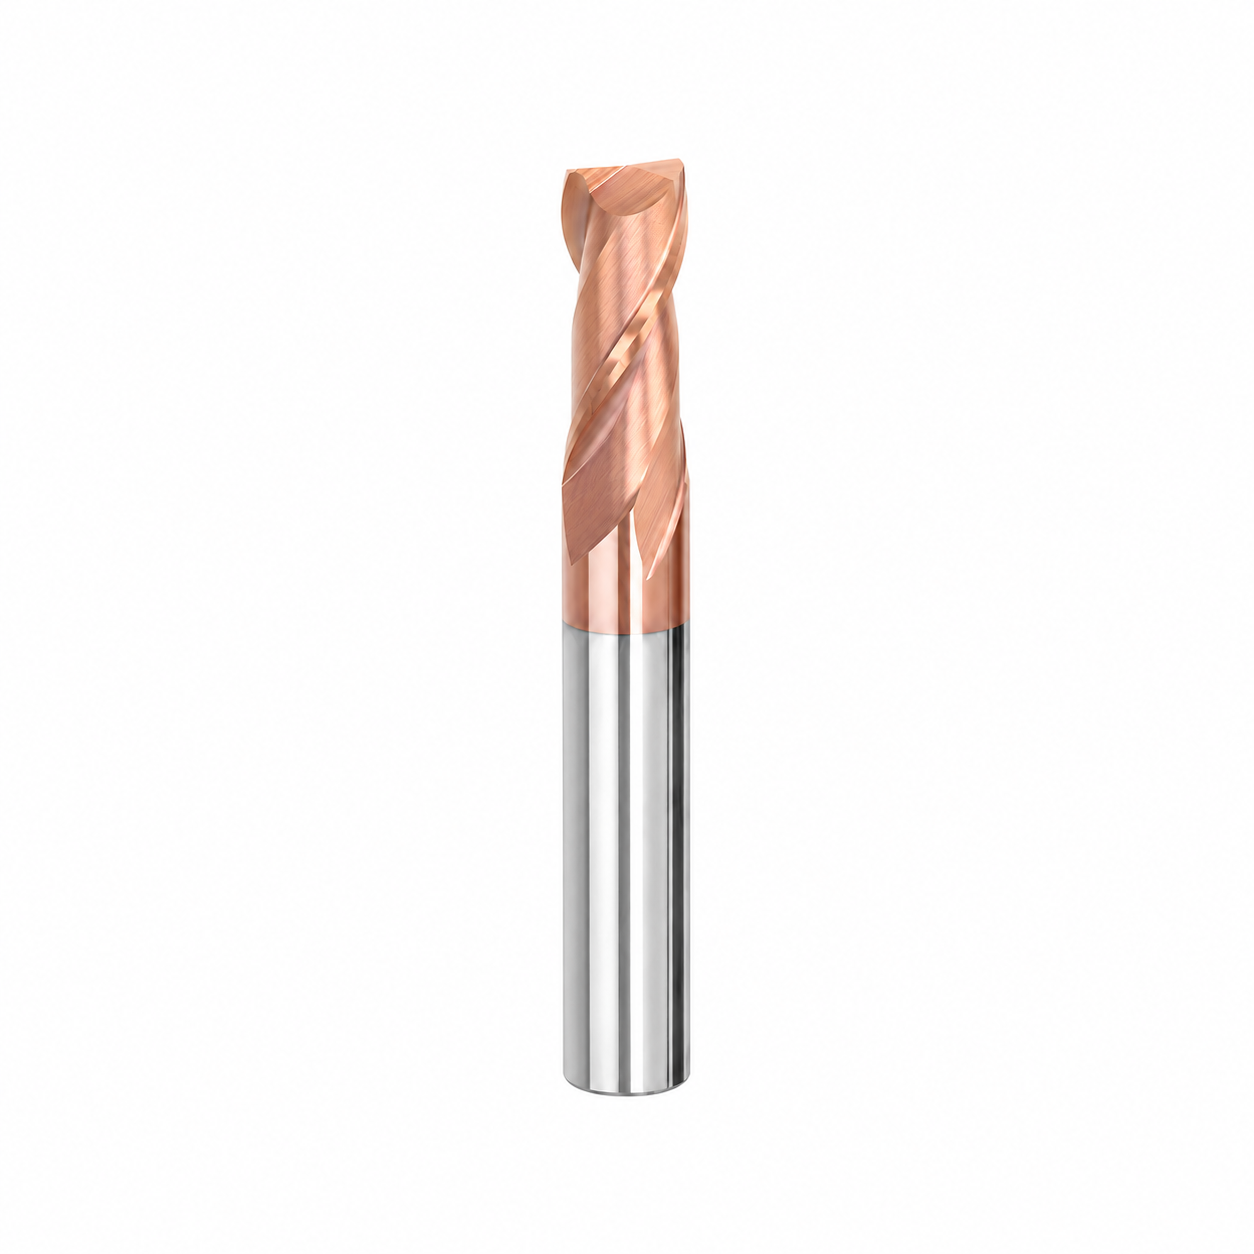
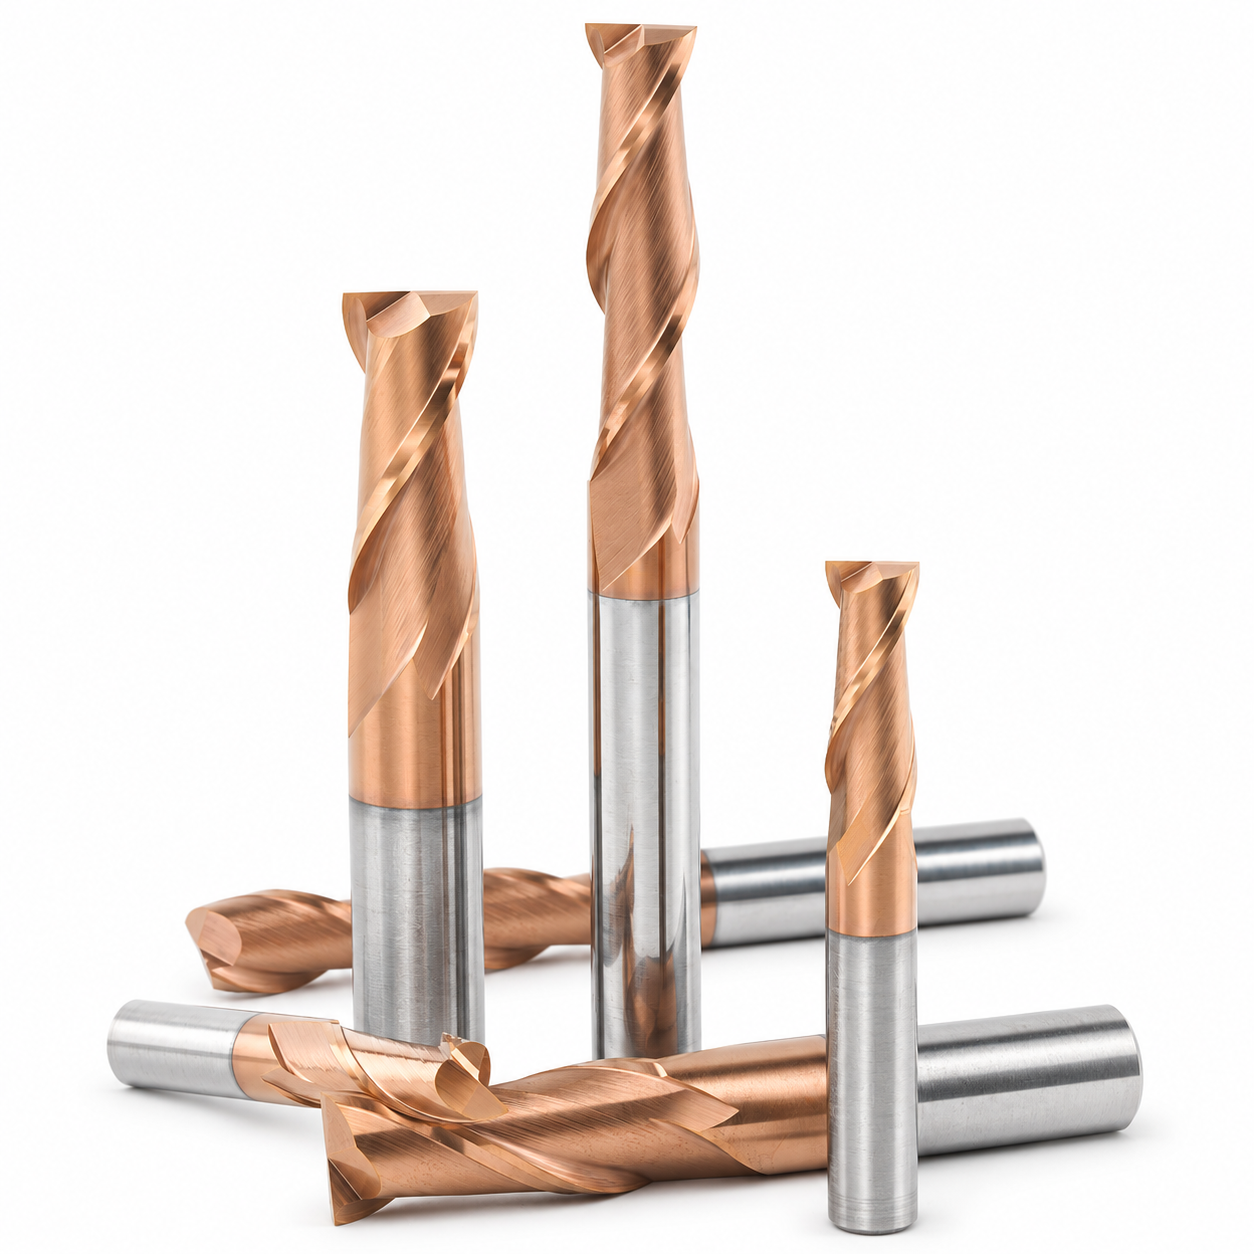
HRC55 2 Flute TiSiN Coated Solid Carbide Square End Mill
Our HRC55 2-flute solid carbide square end mills (also known as flat end mills or carbide milling cutters) feature a wear-resistant TiSiN coating for CNC machining of carbon steel, alloy steel, and pre-hardened steel up to HRC55.
Product Overview
HRC55 TiSiN Coated Solid Carbide Square End Mills for Steel
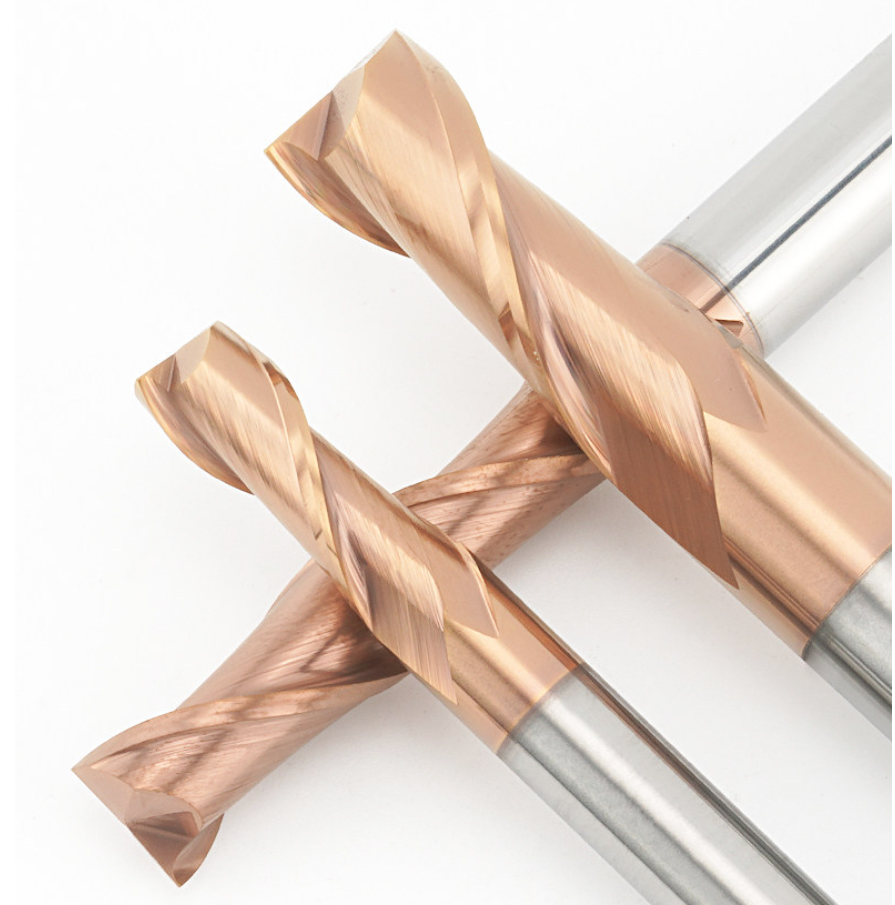
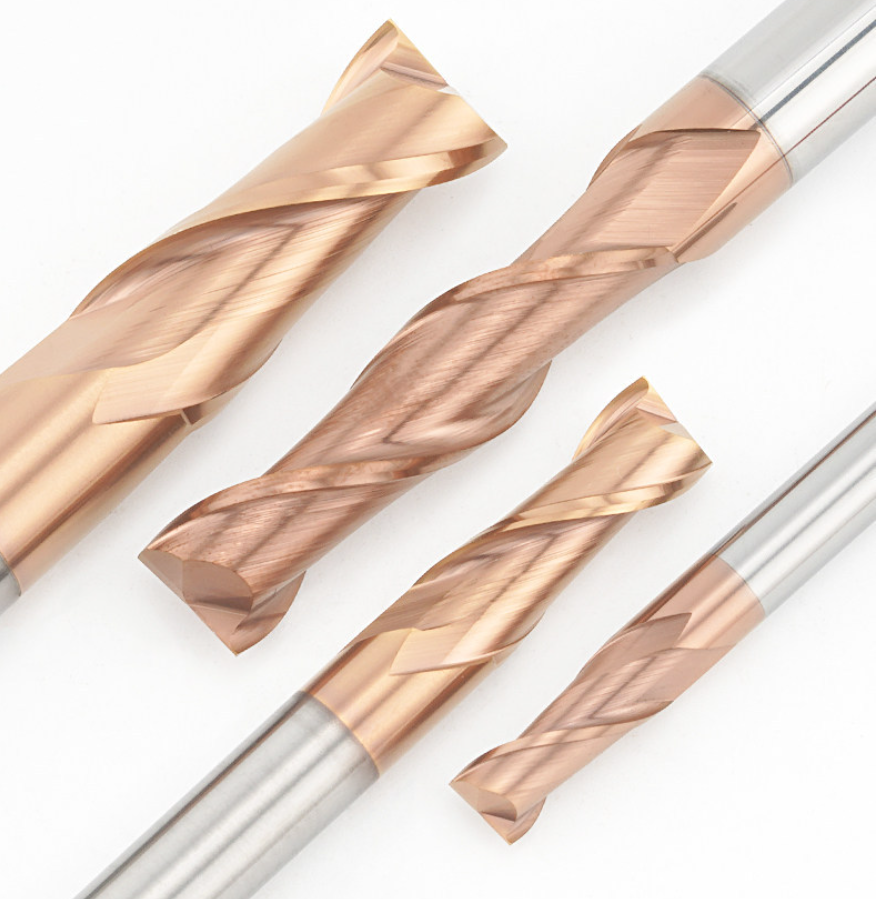
Our HRC55 2-flute solid carbide square end mills (also known as flat end mills or carbide milling cutters) feature a wear-resistant TiSiN coating for CNC machining of carbon steel, alloy steel, and pre-hardened steels up to HRC55. The two-flute cutting geometry provides chip clearance for slotting, side milling, profiling, and general-purpose steel machining, while the TiSiN coating helps improve wear resistance and cutting-edge durability.
Available in a wide range of cutting diameters, flute lengths, shank diameters, and overall lengths, these coated carbide end mills offer flexible size options for different machining requirements, with custom sizes and OEM/private-label support for distributors and tooling suppliers.

Specifications & Cutting Data
Technical Specifications
| Parameter | Specification |
|---|---|
| Tool Material | Solid Carbide |
| Flutes | 2 |
| End Type | Square (flat) |
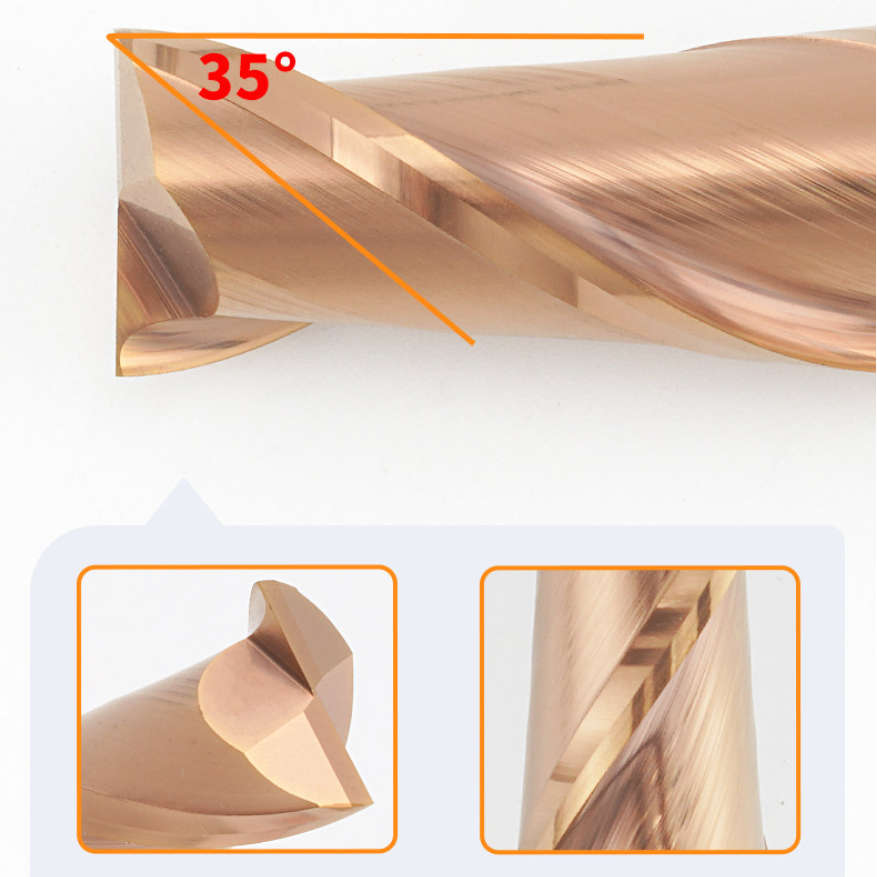
| Helix Angle | 35° |
| Coating | TiSiN |
| Workpiece Hardness | Up to HRC55 |
| Shank Type | Straight Shank |
| Primary Applications | Steel milling, slotting, keyway milling, profiling |
Dimensions & Available Sizes
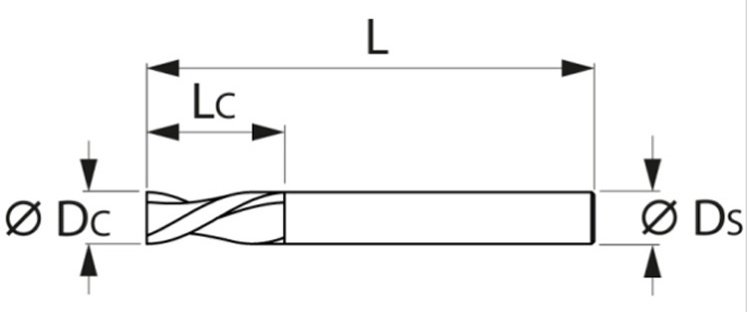
All dimensions in mm. 25 size combinations shown. Please confirm availability before ordering.
| Cutting Ø (Dc) | Flute (Lc) | Shank (Ds) | OAL (L) |
|---|---|---|---|
| 1 | 3 | 4 | 50 |
| 1.5 | 5 | 4 | 50 |
| 2 | 6 | 4 | 50 |
| 2.5 | 8 | 4 | 50 |
| 3 | 9 | 3 | 50 |
| 3 | 9 | 4 | 60 |
| 3.5 | 11 | 4 | 50 |
| 4 | 12 | 4 | 50 |
| 5 | 13 | 5 | 50 |
| 5 | 13 | 6 | 50 |
Show 15 more sizes (25 total)
| Cutting Ø (Dc) | Flute (Lc) | Shank (Ds) | OAL (L) |
|---|---|---|---|
| 6 | 15 | 6 | 50 |
| 7 | 20 | 8 | 60 |
| 8 | 20 | 8 | 60 |
| 9 | 25 | 10 | 75 |
| 10 | 25 | 10 | 75 |
| 10 | 30 | 10 | 75 |
| 11 | 30 | 12 | 75 |
| 12 | 30 | 12 | 75 |
| 12 | 35 | 12 | 75 |
| 13 | 45 | 14 | 100 |
| 14 | 45 | 14 | 100 |
| 15 | 45 | 16 | 100 |
| 16 | 45 | 16 | 100 |
| 18 | 45 | 18 | 100 |
| 20 | 45 | 20 | 100 |
Workpiece Materials
P
Suitable Workpiece Materials
Alloy Steel
Pre-Hardened Steel (up to HRC55)
K
Suitable Workpiece Materials
Selected High-Alloy Cast Iron
Cutting Data Reference
Reference cutting data only; not tool-tested. Adjust for material hardness and machining conditions.
ap = axial depth, ae = radial width, D = tool diameter. n (rpm) = Vc × 1000 ÷ (π × D).
| ISO | Workpiece Material | Reference Condition | Vc (m/min) | ap | ae |
|---|---|---|---|---|---|
| P | Carbon / Alloy Steel | Below HRC45 | 180 | ≤ 1.5D | ≤ 0.15D |
| P | Alloy Steel | HRC50 | 130 | ≤ 1.0D | ≤ 0.12D |
| K | Gray Cast Iron | Under HRC32 (source chart) | 160 | ≤ 1.5D | ≤ 0.15D |
| K | High-Alloy Cast Iron | HRC35–45 (source chart) | 140 | ≤ 1.0D | ≤ 0.12D |
For steel above HRC50 and for cast-iron grades, cutting parameters require confirmation.
For full-width slotting, use 50–70% cutting speed and 40–60% feed rate of side-milling values. Vf (mm/min) = n × 2 × fz.
On mobile, swipe the tables sideways to see all columns.
Send your required sizes, quantities, workpiece material and destination for wholesale pricing and delivery options.
Customization & OEM Supply
We provide custom sizes, tool geometry modifications, and OEM/private-label solutions for our HRC55 2-flute TiSiN-coated solid carbide square end mills. Distributors and tooling suppliers can tailor tool specifications, laser marking, and packaging to meet their machining needs and brand requirements.
Custom Tool & Branding Options
| Cutting Diameter | Standard & special diameters |
|---|---|
| Tool Dimensions | Flute length, shank diameter & overall length |
| Coating | TiSiN / Custom on request |
| Laser Marking | Your logo, tool size & product code |
| Private Label | Individual tool packaging & custom labels |
| Minimum Order | 10pcs Per Size |
| Custom Lead Time | In-stock: 1–3 days; custom orders: subject to confirmation |
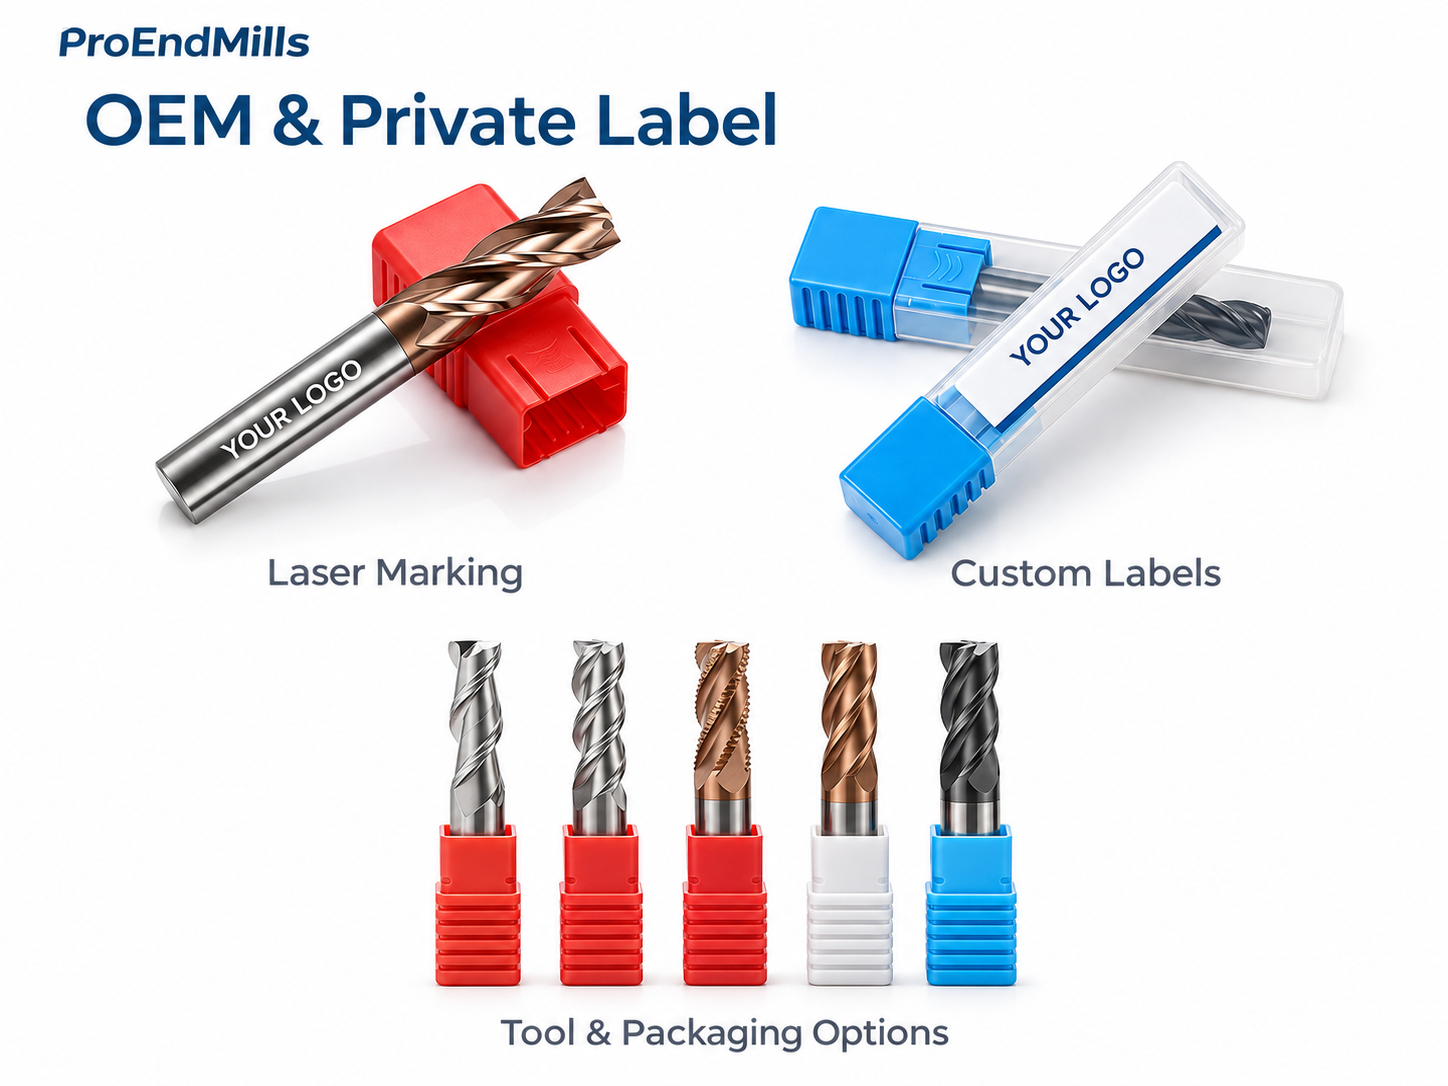
OEM branding illustration. Final details confirmed with your order.
Quality, Ordering & Delivery
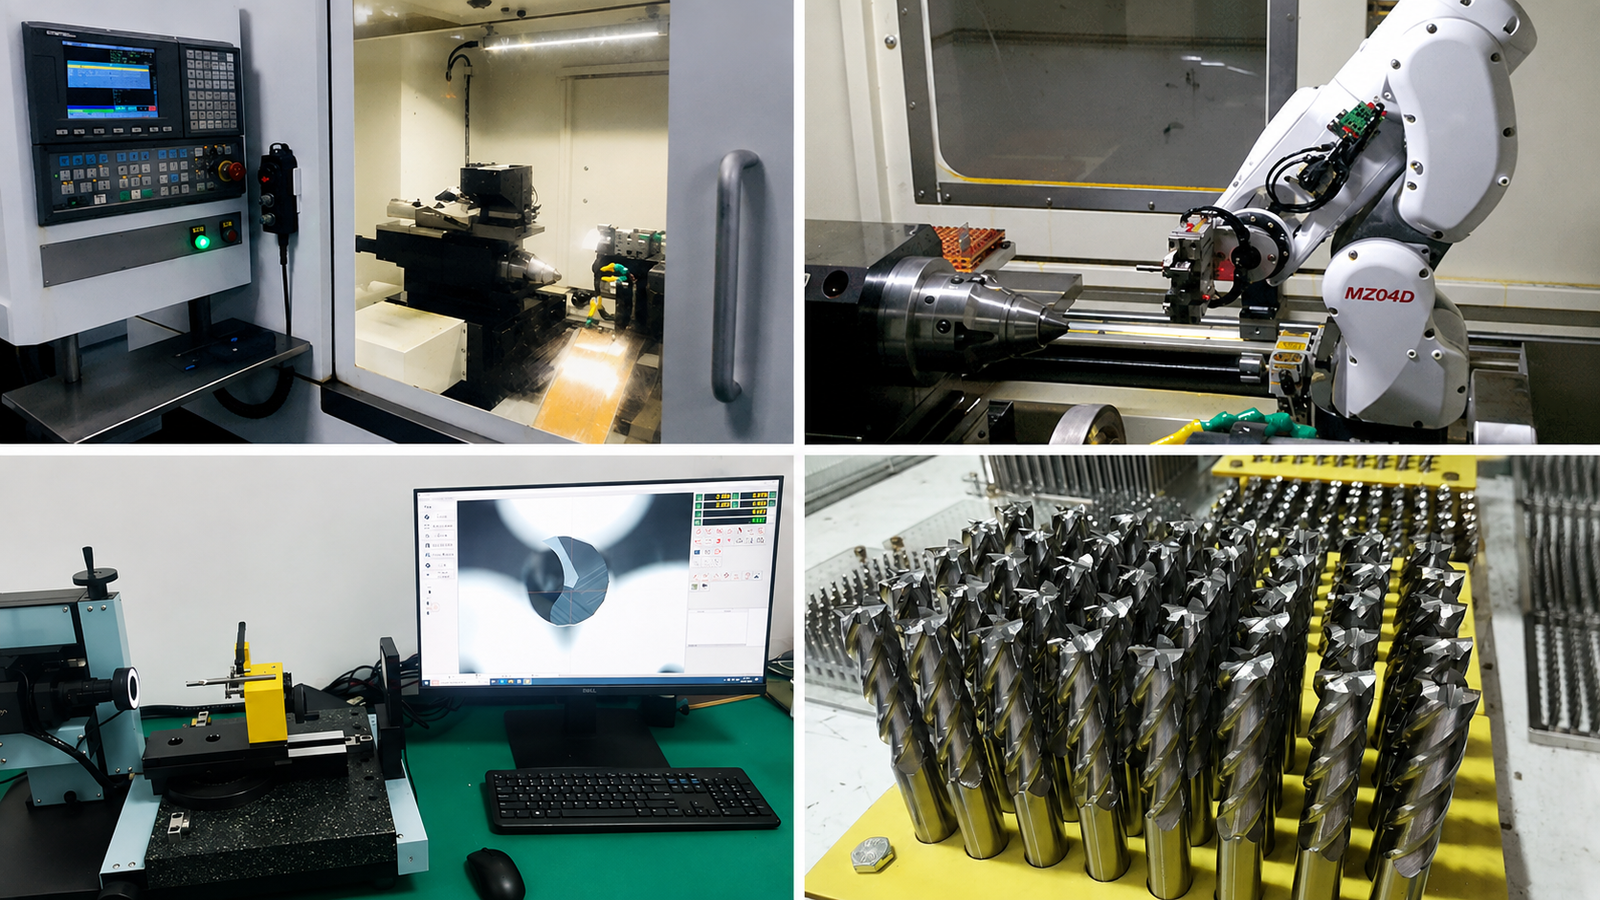
Manufacturing & Quality Checks
Ordering & Delivery
* Custom lead times, shipping costs and DDP availability are subject to confirmation.
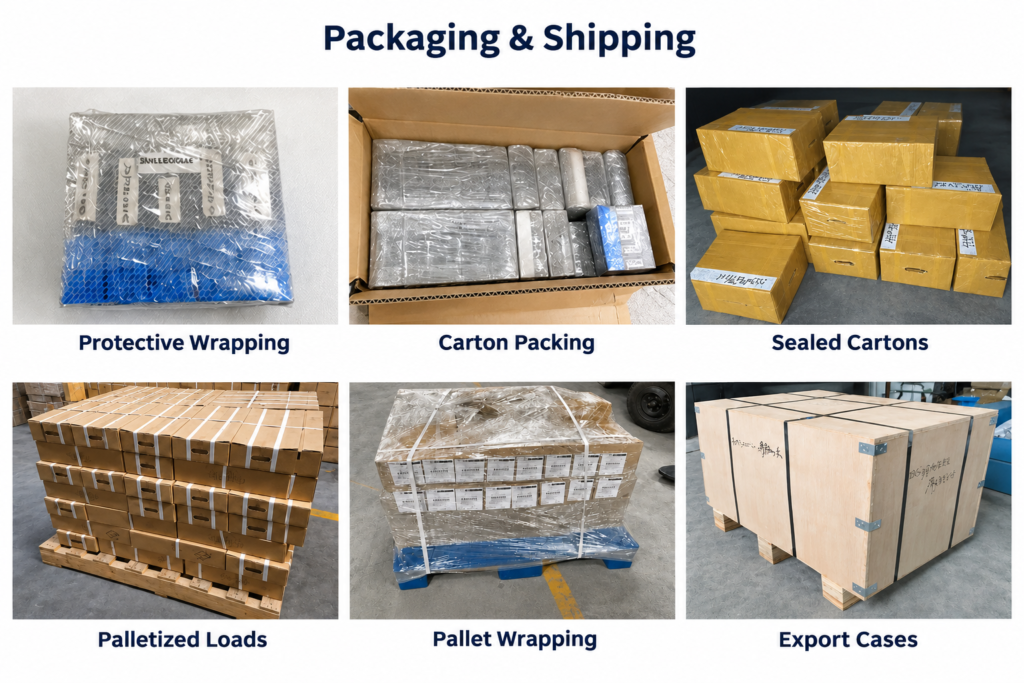
Protective Packaging
Our carbide end mills are individually packed and protected for international shipping, with additional reinforcement available for bulk orders.
FAQ
Request Pricing & Availability
Send your required sizes and quantities for a quotation.
- Standard Sizes
- Trial Orders
- Mixed Sizes
- Custom & OEM